
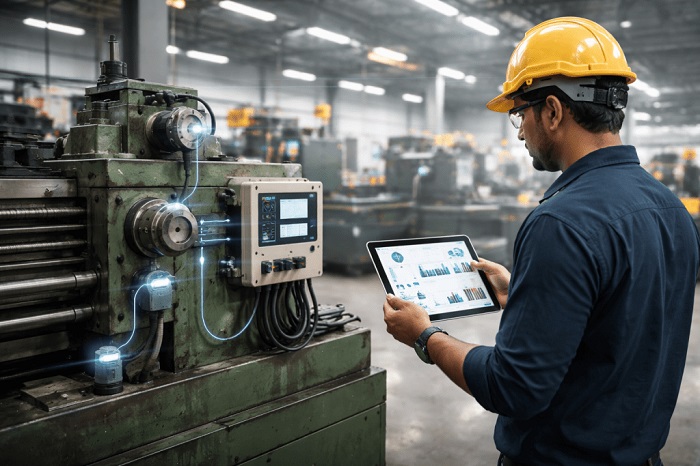
Walking into an established manufacturing plant often feels like stepping across two different technological eras. On one end of the floor, high-precision robotic cells and multi-axis CNC machines hum with high-speed efficiency. On the other end, tucked inside a climate-controlled control room, sits a faded desktop running a supervisory control and data acquisition (SCADA) platform installed twenty years ago. The interface features dated graphics, runs on an unsupported operating system, and relies on proprietary drivers that no living vendor representative remembers writing.
Plant managers and operations directors understand the acute vulnerability of this setup. Legacy SCADA systems introduce severe cybersecurity risks, lack compatibility with modern enterprise resource planning platforms, and depend on obsolete hardware that could fail without warning. Yet, the upgrade project remains stalled on the annual capital expenditure docket. The hesitation is rarely financial; it is rooted in fear. In an environment where an hour of unplanned downtime can cost tens of thousands of dollars, the prospect of taking a production line offline to deploy new supervisory software feels like an unacceptable gamble.
Modernizing operational technology does not require a reckless leap of faith. By shifting away from the traditional, all-at-once migration and adopting an incremental, phased approach, industrial facilities can deploy modern SCADA architectures without interrupting day-to-day throughput.
The Flaws of the All-at-Once Migration
The conventional approach to software updates in enterprise environments relies on the cutover: shutting down the old system on a Friday evening, running an intensive deployment over the weekend, and expecting operators to run production by Monday morning. In discrete manufacturing or continuous process environments, this methodology frequently collapses.
Industrial automation is tied to physical physics and timing-dependent field operations. A legacy SCADA deployment is not just a user interface; it is an intricate web of programmable logic controller (PLC) routines, hardwired remote terminal units (RTUs), custom calculation scripts, and analog communication loops. When teams attempt an immediate cutover, undocumented dependencies surface under pressure. A timing discrepancy in a polling cycle, an unmapped setpoint, or an unexpected communication timeout can leave an entire packaging or chemical processing line non-responsive.
When teams fall behind schedule during a weekend deployment, leadership faces an agonizing choice: spend millions waiting for engineering teams to troubleshoot undocumented logic, or roll back the installation and write off months of preparation. This binary risk is why modern engineering teams have abandoned the single-event conversion model altogether.
Phase 1: Comprehensive Asset Discovery and Tag Auditing
Every successful SCADA modernization begins with digital reconnaissance. Over decades of operational changes, SCADA tag databases accumulate massive amounts of technical debt. Engineers patch code during emergency shutdowns, add temporary override scripts that become permanent, and abandon obsolete sensors without removing their associated tags from the polling cycle.
Before evaluating modern software platforms, automation teams must execute a thorough inventory of the existing supervisory layer:
-
Hardware and Physical Media Mapping: Document every physical connection, including legacy serial connections (RS-232, RS-485), proprietary industrial networks (Data Highway Plus, Modbus RTU, Profibus), and legacy network switches operating at levels 1 and 2 of the Purdue Model.
-
Tag Database Sanitization: Categorize active versus inactive tags. Determine which tags actively drive alarms, control loops, and batch recipes, and flag orphaned tags that consume network bandwidth without delivering operational value.
-
Script and Logic Extraction: Identify proprietary macros, legacy Visual Basic scripts, and custom SQL queries embedded within the old supervisory interface. These custom routines often contain critical plant logic that is missing from formal engineering documentation.
This discovery process establishes a verifiable baseline. It clarifies the scope of the project and prevents the migration of useless, disorganized data into the new platform.
Phase 2: Parallel Architecture and Non-Intrusive Data Tapping
The core mechanism for eliminating downtime during an upgrade is building the new SCADA platform alongside the operational legacy system, rather than in place of it.
Modern industrial architectures thrive on edge gateways, open standards, and decoupled communication layers. By deploying edge appliances or secondary communication cards into existing rack-mounted PLCs, engineers can establish read-only data pipelines directly to the new platform. Technologies like OPC UA and MQTT with Sparkplug B definitions allow plant teams to collect telemetry from legacy controllers without altering the existing polling loops that keep the physical line moving.
During this stage, the legacy SCADA continues to handle all real-time operator control, supervisory setpoint transmission, and safety alarms. Meanwhile, the new platform ingests the identical data stream in the background. This architecture allows engineering teams to construct screens, test database performance, and configure alarm matrices without placing the physical production line at risk.
Phase 3: Dual-Run Shadowing and Modular Commissioning
Once the parallel platform is established, the project enters a verification period known as shadow operations. During this phase, engineering teams run both systems simultaneously, comparing real-time operational states across both platforms to identify discrepancies.
Telemetry Reconciliation and Alarm Rationalization
Shadow running allows engineers to verify that raw analog values, scaling factors, and calculation scripts translate accurately into the new environment. If a temperature transmitter registers 450 degrees Fahrenheit on the legacy screen but displays a scaled variance on the new interface, the root cause can be isolated and resolved during normal working hours without disrupting operators.
This stage also presents the prime opportunity to resolve alarm fatigue. Using standards like ISA-18.2, teams can systematically audit historical alarm frequencies, eliminate nuisance alarms, and structure warning priorities before the new screens go live.
Sectional Cutover During Planned Maintenance
Rather than flipping the entire facility over in a single shift, deployment should follow a modular sequence aligned with regular maintenance intervals. A multi-stage facility can migrate utility systems first—such as chillers, compressed air, and wastewater treatment—where short-term control interruptions carry lower operational consequences.
Once utility integrations prove stable, teams proceed to primary production cells one at a time. Each cell transition takes place during standard tooling changes or planned preventative maintenance windows, maintaining complete production schedules across the rest of the facility.
Phase 4: Ergonomic Handover and Fail-Safe Governance
The technical success of a control system means little if the human operators on the floor struggle to use it. Early operator involvement is vital for smooth change management.
Modern SCADA design emphasizes situational awareness over cluttered visual schemes. Moving from bright, multi-colored vintage graphics to high-performance HMI standards (such as ISA-101) can initially disorient operators who are accustomed to looking for specific visual cues. By placing new parallel workstations in the control room weeks before the operational cutover, operators have the opportunity to interact with the screens, provide feedback on layout ergonomics, and build familiarity without production pressure.
Finally, every cutover window must be backed by an uncompromising rollback protocol. Before any command-writing authority is transferred to the new system, engineers must establish a clear time limit. If unexpected communication errors or hardware misalignments cannot be resolved within a pre-defined window, the team reinstates control to the legacy system, preserving the production schedule and deferring the shift to the next planned window.
Treating a SCADA migration as a phased, parallel engineering program removes the operational volatility that usually stalls infrastructure investments. By decoupling data collection, validating calculations in shadow mode, and migrating processes in manageable cells, manufacturers can eliminate technical debt, enhance operational security, and step securely into modern manufacturing without sacrificing plant output.
Comments are closed.